Quality Assurance & Technical Support
Standardized ASTM and ISO laboratory test protocols ensuring compound consistency, along with comprehensive material selection guidance.
Precision Property Characterization
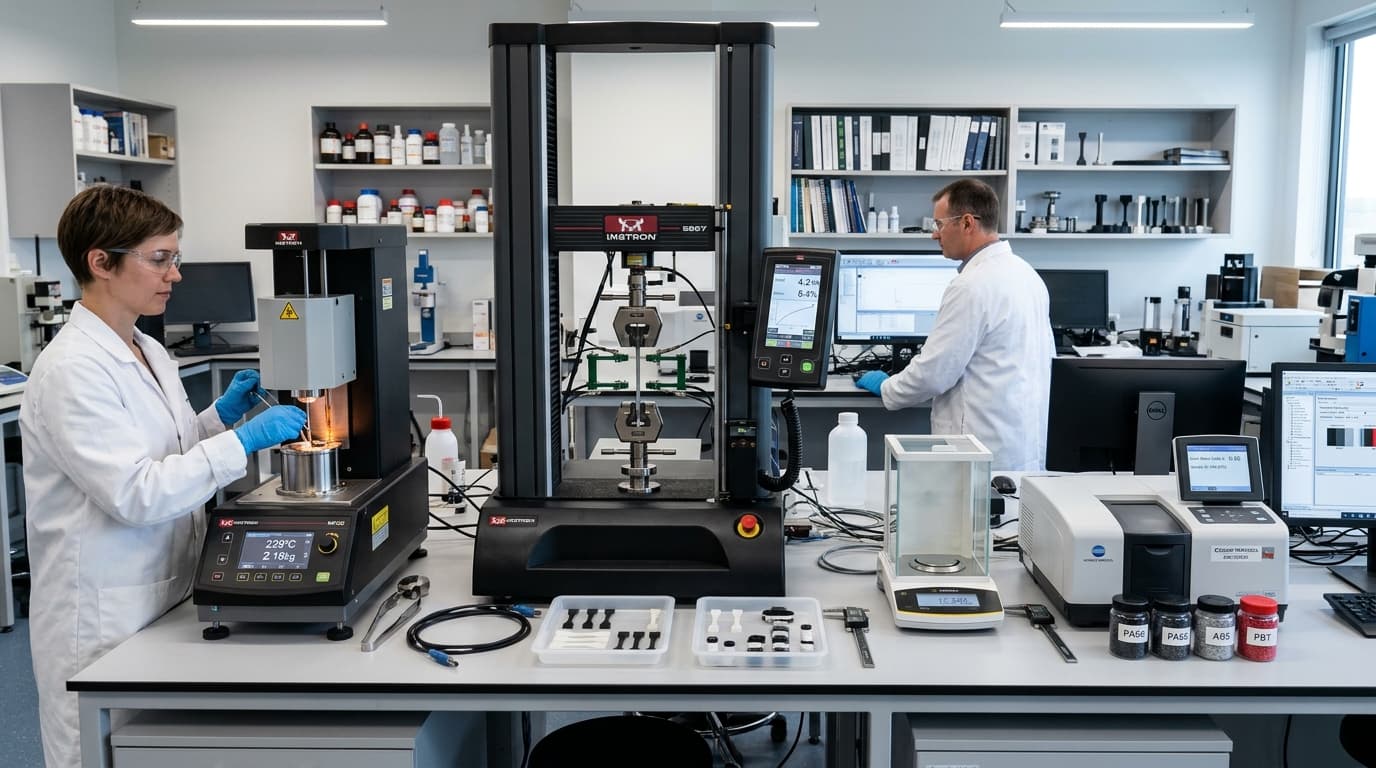
Compounding engineering thermoplastics requires constant laboratory surveillance. At ANNEX, we test incoming polymers, monitor twin-screw melt homogenization, and test injection-moulded standard test bars per international standards.
Melt Flow Index (MFI / MFR)
ASTM D1238 / ISO 1133 melt volume rate verification ensuring mold filling predictability.
Universal Tensile & Flexural Testing
Tensile modulus, elongation at break, and flexural stiffness per ASTM D638 / D790.
Flammability Verification (UL 94)
Vertical and horizontal burn chamber tests for V-0, V-1, V-2, and HB compliance validation.
Ash Content & Filler Verification
High-temperature muffle furnace ash burn tests confirming exact glass fibre loading percentages.
Not Sure Which Material You Need?
Answer a few quick questions regarding your component environment and target properties. Our engineering team will review your specifications and recommend the most optimal thermoplastic compound.
Step 1: Your Application & Component
Tell us what you are moulding or manufacturing.
How We Collaborate on New Moulding Projects
From initial application review to pilot trial lots and series commercial compounding.
Application Review
We review component drawings, gate locations, continuous temperature, mechanical stress, and fire safety directives.
Candidate Grade Proposal
Our application engineer proposes candidate polymer compounds (or standard trading grades) with complete TDS data.
Pilot Sampling Lot
We formulate a 25kg - 100kg trial lot for tool trials on your injection molding machine, adjusting melt viscosity if needed.
Commercial Production
Upon dimensional and mechanical sign-off, series batch production begins with identical compounding screw configurations.